Tabber Stringer Machine Manufacturer: How to Vet One
Table of Contents
Quick answer: Most tabber stringer quotations look alike, so the supplier is the part you can actually inspect. A real manufacturer will accept your own cells for a trial and return EL images, a breakage figure and peel-strength data measured on those cells before you pay a deposit. It will name the cell formats the machine has already run in production, give you a customer running the same format, and state spare-parts lead times in writing. A trading company usually cannot do any of that, because it forwards your questions to a factory you never meet. Three things decide how this ends: who builds the machine, who commissions it on your floor, and who answers when a recipe drifts at two in the morning. Get all three into the quotation, not into the argument after the deposit.
How to separate a tabber stringer machine manufacturer from a reseller, what an acceptance test has to prove, and the quotation details that predict who shows up after commissioning.
PV Module Production · Supplier Evaluation · by Jerry, Ooitech
I have watched enough stringer handovers to know the pattern. The machine lands, it runs, and the first cell format change reveals whether you bought a manufacturer or a middleman. This is how to find that out before the deposit clears.
Start With the Question Buyers Skip
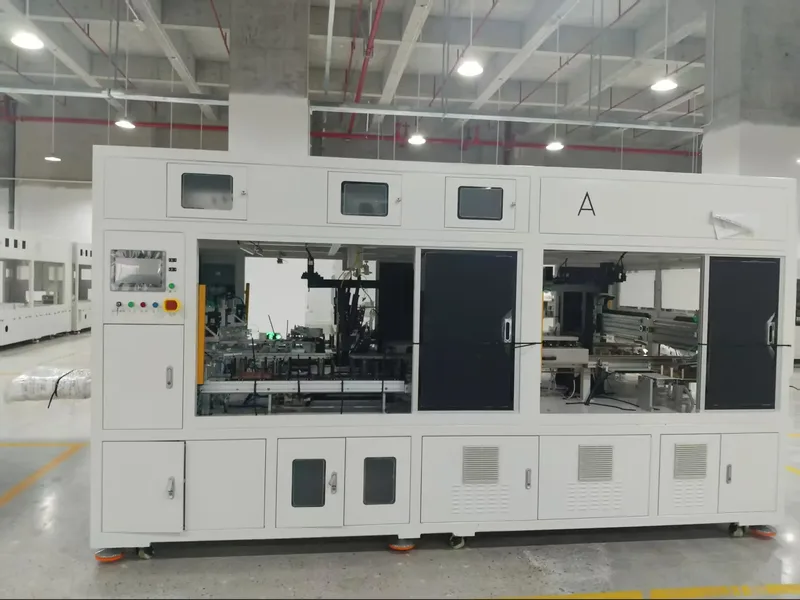
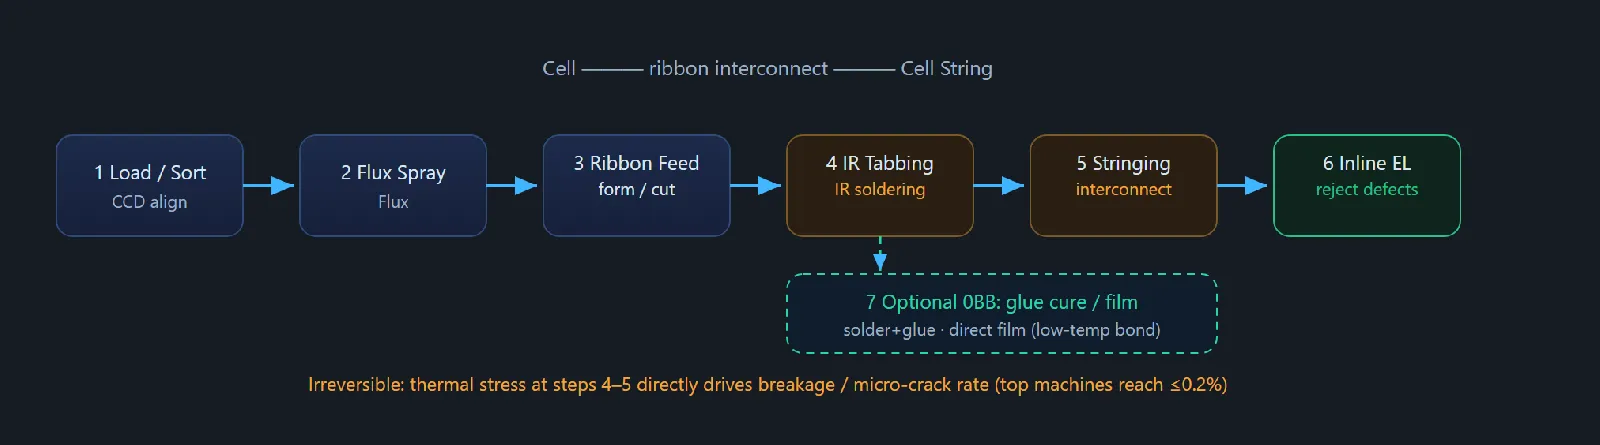
Almost every stringer enquiry I receive opens with throughput or price. Almost none opens with who actually builds the machine. That is backwards, because on this particular station the hardware is the easy part. The six-station IR platform is a solved design, and every serious supplier can show you a machine that solders ribbon to a cell. What varies is everything wrapped around it: whether the recipe library you need exists yet, whether the person who tuned the heating profile for your cell format is reachable in month four, and whether a spare ribbon-feed assembly arrives in two weeks or two months.
Stringing is also the first irreversible step on the line. A crack or a cold joint created here is inside the module forever, so the cost of choosing badly is not the machine price. It is the yield you never reach and the warranty claims you meet in year three. That asymmetry is why supplier evaluation deserves more of your diligence than the specification table does.
If you want the machine-side picture first, the tabber and stringer machine guide covers the stations, soldering method, busbar formats and price bands. This page is about the other half of the decision.
Manufacturer or Trading Company: Four Ways to Tell
Buying through a trading company is not automatically wrong. For a laser cutter or a tape sticker, a competent reseller with local stock can be the better call. A stringer is different, because the machine only works as well as the process recipe tuned to your cells, and that tuning is engineering support rather than a part number. Working through a reseller is defensible when you already run the format and only need delivery. It is a poor fit when you are starting a line, changing cell technology, or tolling for several customers.
| What you ask for | What a manufacturer answers | What a reseller answers |
|---|---|---|
| Where is the machine assembled | A plant address, and usually an invitation to visit it and see the station running | A partner factory, named late or vaguely, with the visit routed through them |
| Can you change a specification | Yes, with an engineering reason, a cost delta and a delivery impact stated separately | “Standard machine”, or a change order that takes a week to price |
| Who tunes the heating recipe | The same engineers who built and tested the platform, on your cells | A commissioning subcontractor, or a remote call with the factory |
| Spare parts and lead time | A parts list with lead times, because they hold the assemblies | “We will check with the factory”, which is the answer you will keep getting |
There is a faster test than any of those. Ask for the name and contact of one customer running your exact cell format, and say you want to speak to their process engineer rather than their purchasing manager. A manufacturer usually produces one within a day, because they know who runs what. A reseller asks you to submit the question in writing and returns a reference you are not permitted to contact directly. Note how long the first reply takes.
What an Acceptance Test Must Prove
A stringer trial that runs on the supplier’s own cells proves very little. Their cells are selected, their recipe is already dialled in for them, and the machine is warm. The test worth travelling for is the one you design: send a pallet of your production cells, including the ones you worry about, and ask for measurements rather than impressions.
Bring the awkward cells on purpose. Half-cut N-type wafers at the thin end of your supplier’s stated thickness range, cells from a batch with known edge chips, and at least one format you plan to run next year rather than this year. A machine that handles your best cells is table stakes; the useful signal is where it starts producing microcracks.
- Breakage and microcrack count from in-line EL, on your cells, with the EL images handed over rather than summarised.
- Peel strength figures from a pull test on strings made from your cells, not a reference value from a datasheet.
- The heating recipe that produced those results, exported as a file you keep, so the starting point is documented on day one.
- Changeover time between two of your formats, measured with a stopwatch during the trial rather than quoted afterwards.
If a supplier will not let you send cells, or will only show you a machine running their own stock, treat the specification table as marketing until it is proven otherwise. This is where most of the risk in a stringer purchase sits, because in a normal contract the machine is commissioned and paid for before your own cells ever run through it.
The Spec Sheet Test
You can judge a supplier by how completely they fill in a specification table. Vague quotations are not a stylistic choice; they are a hedge, and every blank becomes a change order later. A complete stringer specification answers at least these: rated capacity per cell type, positioning and placing accuracy as separate figures, breakage rate with the cell grade it was measured on, the ribbon width and thickness window, maximum string length, the control architecture, and whether in-line EL is standard or an option.
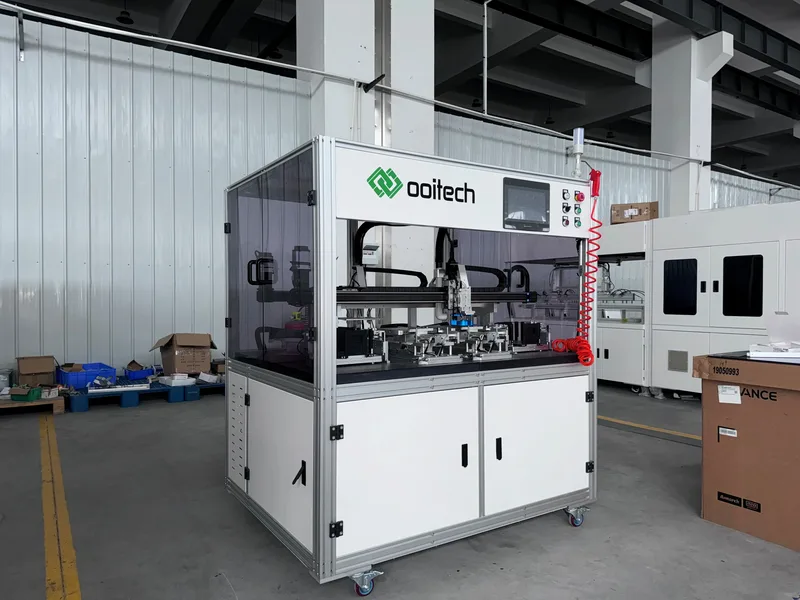
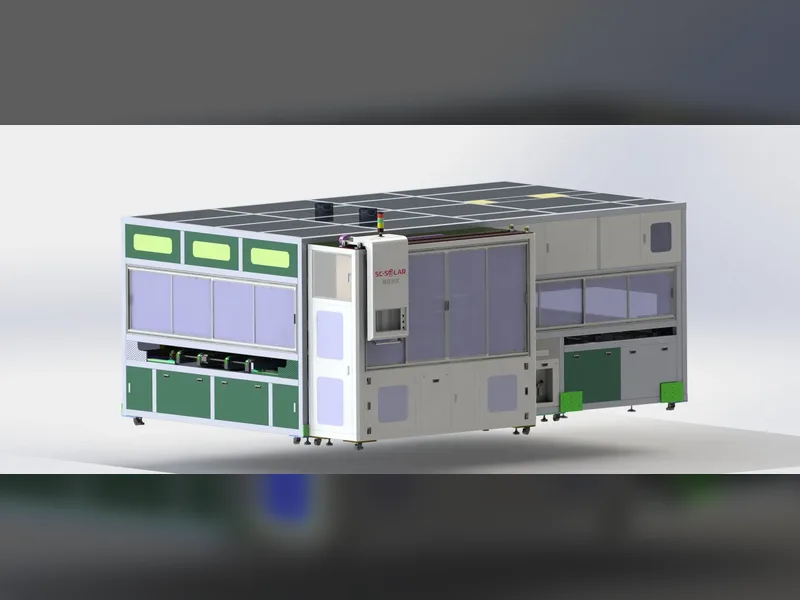
Here is the table for our entry-class machine, published in the same shape we give it to buyers, so you can hold any quotation against a filled-in example. Ours is the SS-1500B, which we configure without the gluing function as standard.
| Parameter | Specification |
|---|---|
| Capacity | BC cells 1000 pcs/h; TOPCon and PERC cells 1200 pcs/h |
| Positioning accuracy | ±0.15 mm |
| Placing accuracy | ±0.2 mm |
| Cell fragmentation rate | ≤0.2%, measured on Class A cells |
| Equipment failure rate | ≤3% — a machine-availability figure, not a breakage figure |
| Cell size | 166–210 × 30–166 mm |
| Ribbon (flat) | Width 0.35–1.0 mm, thickness 0.12–0.25 mm |
| Maximum string length | 1800 mm |
| Welding method | Infrared lamp with ribbon welding |
| Cell detection | CCD camera system, fully automatic loading and unloading |
| Control architecture | PLC with servo, CCD, robot handling and touchscreen HMI |
Two rows in that table are worth dwelling on, because they are the ones most often blurred in a quotation. Fragmentation rate and equipment failure rate are different numbers with different consequences: the first costs you cells, the second costs you output hours. If a supplier offers a single percentage without naming which one it is, ask which of the two it is. Suppliers who answer immediately, with the test condition attached, are usually the ones whose other figures are worth checking too. The SS-1500B specification page carries the full parameter set, and the SS-2500B covers the higher-capacity class if your line rate needs it.
Cell Kits, Recipes and the Cost of a Second Format
Most lines end up running more formats than they planned. A buyer who starts on 182 mm PERC adds half-cut TOPCon within two years, and a tolling operation may hold four formats live at once. Whether that is a scheduling inconvenience or a capital problem depends entirely on what you bought up front, so this belongs in the original negotiation rather than in a later upgrade order.
Ask what a complete cell kit contains, how many ship with the machine, and what a second kit costs if you order it with the machine rather than afterwards. The gap between those two prices is usually wider than buyers expect. Ask too whether recipes are stored per format on the machine and exportable as files. A supplier who treats recipes as operator knowledge rather than as documentation is handing you a single point of failure that walks out of the door at shift end.
Format flexibility is also what makes a machine resellable. A stringer that only ever ran one format has a customer list of one. If your plan includes tolling, or if the cell roadmap in your region is still moving, pay for changeover capability now. Our own AM050FH platform was specified around that problem, combining multi-busbar soldering with laser half-cut and one-third-cut on one frame.
Who Trains Your Operators, and for How Long
Commissioning is not the same as being production-ready, and the gap between them is measured in months. The machine can be capable on the day the engineers leave while your rated yield is still two or three months away, because what you are actually building in that window is a recipe library and an operator’s eye for drift.
So make the support window part of the contract and be specific about it. How many days of on-site commissioning are included, how many engineers come, and what happens on day thirty-one when a new cell batch behaves differently? Some suppliers include a defined remote-support period; others consider the relationship finished at sign-off. Neither is unreasonable, but you need to know which one you bought, because the cost of a stranded recipe falls on your yield rather than on their invoice.
Red Flags in a Quotation
A quotation is a description of a machine, and gaps in it are the most reliable predictor of disputes. When two quotes for the same machine class sit far apart, the difference is rarely generosity; it is scope that quietly left the sheet.
- In-line EL listed as an option rather than standard, with no camera count given.
- Capacity quoted as a single figure with no cell type attached, when BC and PERC rates differ on the same machine.
- No commissioning scope, no training days, and no named support period.
- Cell kits and stored recipes absent from the offer, so format flexibility is priced later at your disadvantage.
- Spare-parts lead times missing, which is the detail that decides how long a stoppage lasts.
- A specification table with more blank cells than filled ones.
None of these make a supplier dishonest. They make a quotation incomplete, and incompleteness is what you argue about six months later. A supplier who volunteers the awkward details, including the ones that raise their own price, is the one worth the deposit. For budget planning by line capacity, our cost breakdown by capacity sets out what the surrounding stations add.
FAQ — Choosing a Stringer Supplier
How do I tell whether a supplier is the actual manufacturer?
Ask for the assembly plant address and an invitation to see the station running, then ask who tunes the heating recipe and who holds the spare assemblies. Manufacturers answer both without routing the question elsewhere. The single fastest check is a reference customer running your cell format, reachable by phone within a day.
What should I send a supplier for an acceptance test?
Your own production cells, including deliberately awkward ones: thin half-cut N-type wafers, a batch with known edge chips, and the format you expect to run next year. Ask for EL images, a microcrack count, peel-strength data and the exported recipe file. A trial on the supplier’s selected cells tells you almost nothing about your line.
Should the stringer and the rest of the line come from one supplier?
Not necessarily, but the interfaces need an owner. Stringer takt has to match the layup and laminator cycle, and when two vendors supply adjacent stations, a mismatch becomes a conversation about whose equipment is at fault. Buying the line together simplifies that. Buying the stringer separately is workable if you or your integrator own the cycle-time calculation and hold both vendors to it.
One quotation is far below the others. What am I missing?
Usually in-line EL, robotic handling, spare cell kits or commissioning scope, in some combination. Ask for the offer restated line by line against a fully specified competitor and see which rows disappear. If nothing disappears and the price still holds, ask what the capacity figure was measured on. Differences that survive that comparison are real.
How long does commissioning and training take?
Mechanical commissioning and recipe validation are separate phases. Expect the machine to run on day one of commissioning, and expect two to three months before the recipe library and operator familiarity support rated yield. Contract the support window to cover that second phase, because that is when the difficult cell batches arrive.
Do I need to buy spare cell kits up front?
If more than one format is in your two-year plan, yes, and buy them with the machine. Kits ordered later cost more and arrive on someone else’s schedule. Also confirm that the recipes for those formats are stored on the machine and exported to you as files, so a changeover does not depend on one operator’s memory.
Final thoughts: judge a stringer supplier on four things you can verify before paying. Do they accept your cells for a trial, do they publish a complete specification including both failure figures, do they name a reference running your format, and do they put a support window in the contract? Everything else in the quotation is recoverable. Those four are not, and the cheapest time to ask is before you have paid anything.
Specifications reference Ooitech machine data. Cell formats, capacity figures and support scope are confirmed per project against your cells and line rate.